
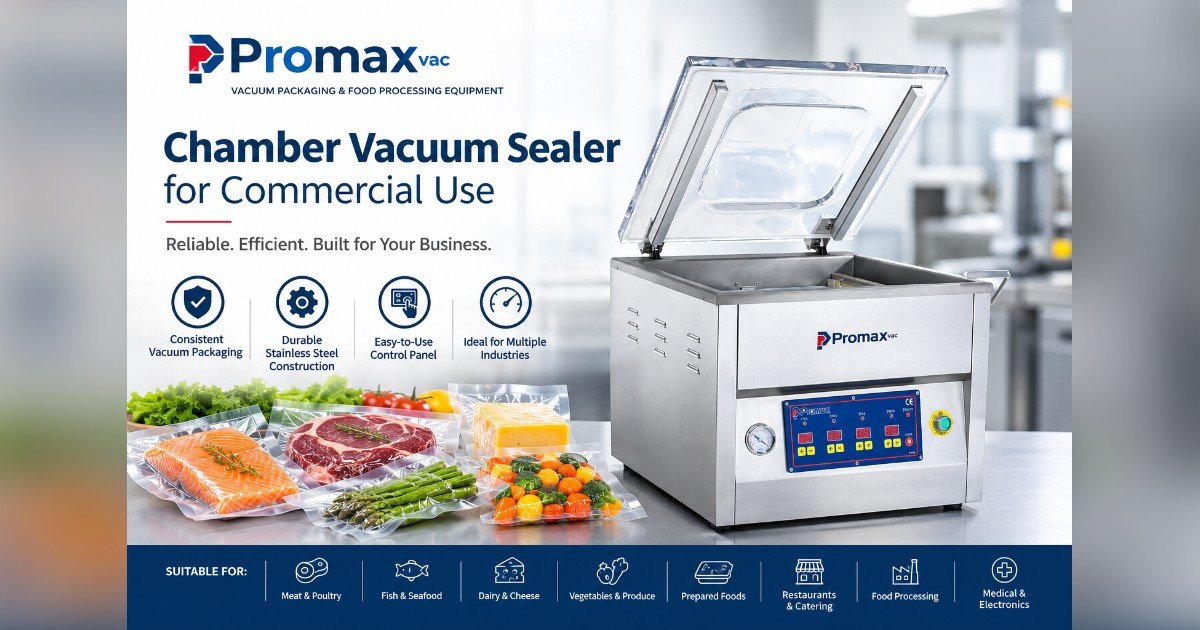
As food processors, distributors, and non-food manufacturers review their packaging lines, the chamber vacuum sealer remains a common choice for operations that need controlled air removal and consistent seals. Promarksvac Corp., a manufacturer of commercial vacuum packaging machines based in Ontario, California, is outlining the factors that typically shape equipment selection in this category. The guidance matters because packaging efficiency and reliability directly affect throughput, product shelf life, and compliance with hygiene standards in commercial settings.
A chamber vacuum sealer places both the product and its pouch inside a sealed chamber. Air is removed from the entire chamber rather than drawn out of the pouch through a nozzle, and the pouch is heat sealed before the chamber returns to normal pressure. Because pressure inside and outside the pouch stays balanced during the cycle, this method is widely used for products containing liquids or moisture, such as marinated proteins, brined products, and prepared meals. This capability is critical for processors dealing with wet or semi-liquid foods, where nozzle-type machines may struggle.
Chamber machines are built in several formats. Tabletop models suit smaller kitchens, retail meat counters, and lower-volume production. Single-chamber floor models are used where larger products or higher daily volumes are involved. Double-chamber designs allow an operator to load one chamber while the other completes its cycle, which can matter in continuous production settings. Belt-type and nozzle-type machines address other workflows within the broader vacuum packaging equipment category. Selecting the right configuration is essential because it determines how well the equipment integrates into existing operations and whether it can accommodate future growth.
Packaging managers comparing commercial vacuum packaging machines generally weigh several practical points: chamber dimensions and seal bar length relative to product and pouch size; pump capacity and cycle time relative to daily volume; compatibility with the pouch material and thickness in use; cleanability and hygiene requirements for the production environment; applicable electrical and sanitation certifications; and availability of spare parts, manuals, and technical support. These factors collectively influence total cost of ownership and operational uptime, making them central to any equipment decision.
Promarksvac Corp. has manufactured vacuum packaging machines and food processing equipment since 1989. The company’s range of industrial vacuum packaging equipment includes tabletop, single-chamber, double-chamber, belt, and nozzle-type machines. Selected systems are equipped with Busch vacuum pumps and are available with applicable UL, ETL, and NSF certifications. The company also offers rollstock packaging machines, MAP tray sealers, commercial shrink tanks, heat sealers, vacuum seal bags, and spare parts. Its processing equipment includes vacuum tumblers, brine injectors, and piston stuffers. Promarksvac equipment is designed for applications involving meat, poultry, seafood, cheese, and ready-to-eat meals, as well as medical and healthcare packaging. Manufactured in the USA and shipped worldwide, the company is the parent of Foodmax, Profood, and the Promarks Heat Seal Division. Product information, machine manuals, and demonstration videos are available at https://promarksvac.com.
For operations evaluating chamber vacuum sealers, the announcement underscores that equipment selection should be driven by specific production requirements rather than generic specifications. With over three decades of manufacturing experience, Promarksvac positions itself as a resource for businesses seeking to align packaging equipment with their operational and compliance needs.